Description
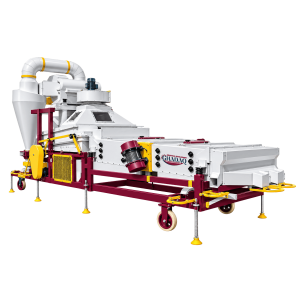
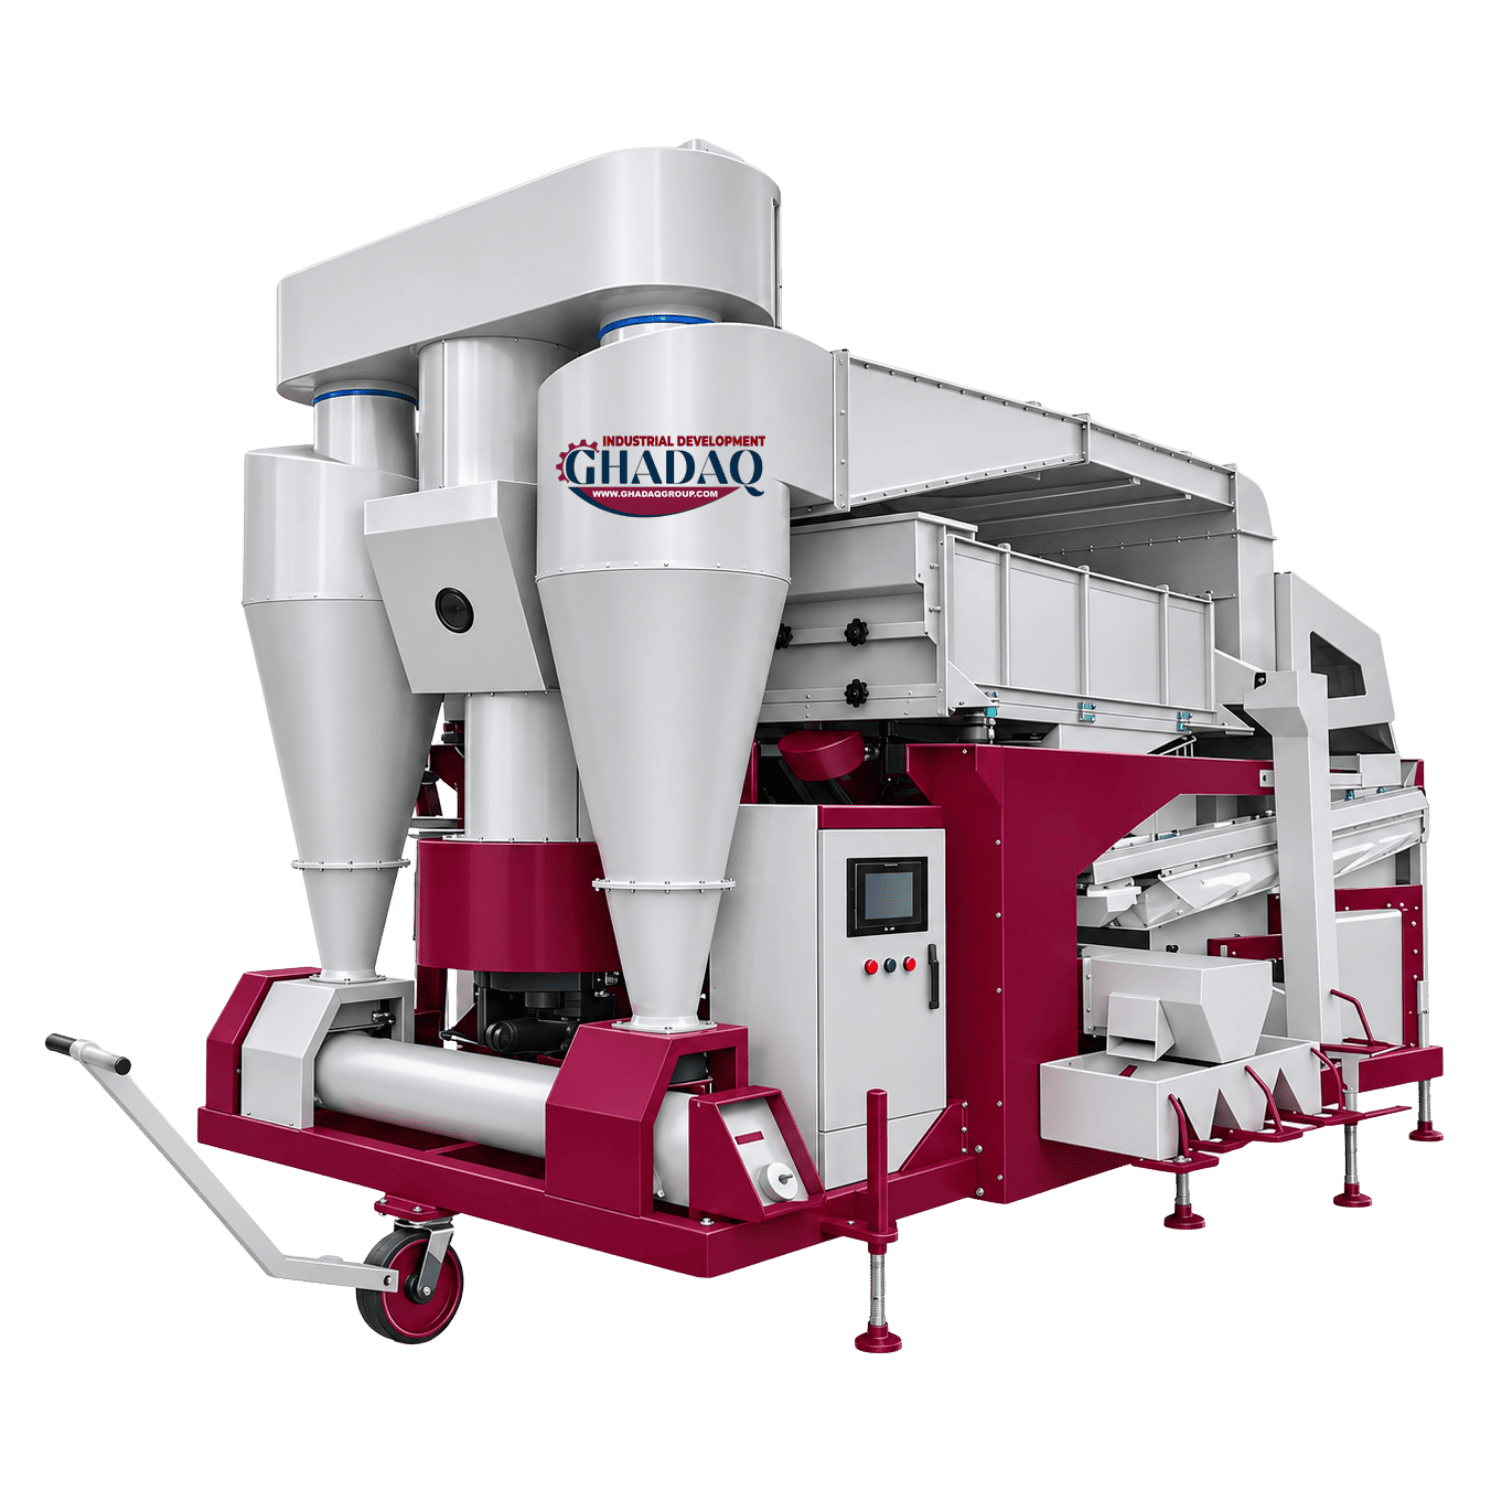
5X ALFA PLUS Compound Gravity Table Seed and Grain Cleaning Machine
The Ghadaq Group 5X ALFA PLUS is a high-capacity industrial machine designed for seed and grain cleaning, separation and grading.
It integrates pre-cleaning, precision screening, air aspiration and specific gravity separation systems within a single structure, offering a comprehensive solution for agricultural product processing.
The machine is intended for industrial seed processing facilities, grain cleaning and grading lines, and agricultural and food industry applications.
Operating Principle
The product is evenly introduced through the machine inlet drum and conveyed by the elevator system to the pre-cleaning unit.
During pre-cleaning, coarse foreign materials are separated from the incoming grain, while the aspiration system removes lightweight particles and impurities.
The material then passes through precision screens, where separation according to particle size is performed.
Finally, the product enters the gravity table unit, which separates grain fractions according to differences in specific weight to improve final product uniformity.
Precision Screening System
The machine is equipped with a two-layer screening system consisting of four pieces in total.
The upper and lower screen sections support the removal of different-sized foreign materials during cleaning.
The vibrating screen measures 1000 × 1500 mm and provides a total screening area of 6.0 m².
The gravity screen measures 2000 × 2250 mm.
High-Capacity Cleaning
Based on wheat, the machine has a fine-cleaning capacity of 15–20 tons/hour and a pre-cleaning capacity of 40 tons/hour.
Processing capacity varies according to the agricultural product. The catalog includes capacity ratings for wheat, rye, barley, oats, corn, rice, soybeans, peas, coffee, sunflower seeds, sesame and selected grass seeds.
Airflow and Drive Systems
The machine incorporates external fans, a gravity bottom fan, a cyclone reducer motor, vibration motors and an elevator inlet motor.
These components support controlled movement through the cleaning stages, air-based impurity removal and gravity separation.
The specified airflow volume for wheat is 17,580 m³/hour.
Key Features and Advantages
- High Processing Capacity: Designed for industrial seed and grain cleaning operations.
- Integrated Cleaning Stages: Combines pre-cleaning, aspiration, precision screening and gravity separation.
- Precision Separation: Separates impurities by size and specific weight.
- Stable Product Flow: Supports consistent movement through the processing system.
- Reduced Product Loss: Designed to minimize kernel damage and product loss.
- Two-Layer Screening: Four-piece precision screening arrangement.
- Efficient Motor and Fan Systems: Designed for energy-efficient operation.
- Robust Industrial Construction: Supports low maintenance requirements and extended service life.
- Uniform Final Product: Helps produce homogeneous, high-quality cleaned grain.
Suitable Products
- Wheat, rye and barley
- Oats and corn
- White rice and rice
- Soybeans and peas
- Coffee beans
- Sunflower seeds
- Rye grass and alfalfa
- Sesame
Applications
- Seed processing plants
- Grain cleaning and grading lines
- Agricultural product preparation facilities
- Agricultural and food industries
- Precision screening and gravity separation systems
Technical Overview
Model: GHA-5XAP-01
Fine-Cleaning Capacity: 15–20 tons/hour
Pre-Cleaning Capacity: 40 tons/hour
Vibrating Screen Area: 6.0 m²
Gravity Screen Dimensions: 2000 × 2250 mm
Machine Weight: 6,800 kg
Ghadaq Group provides integrated high-capacity seed and grain cleaning machinery solutions for industrial agricultural processing facilities.